NATION WIDE LADDER & EQUIPMENT
NH: 603-434-6911MA: 508-754-3030ME: Regular weekly deliveries from NH
- Home
- Blog
Let Nationwide Ladder & Equipment Help You Find What You Need.
How to Choose the Best Vacuum Transfer Pump?
Choosing the right Vacuum Transfer Pump is not simply a matter of comparing catalog prices. The pump must match the fluid, distance, vacuum level, flow rate, temperature, and operating cycle. A unit moving thin solvent behaves differently from one handling viscous oil or abrasive powder. Fit matters. Small leaks hurt.
The U.S. Department of Energy reports that pumping systems can represent about 25% of industrial electricity consumption. This finding, published in Improving Pumping System Performance, shows why efficiency deserves attention before purchase. A pump that reaches the required vacuum quickly may reduce energy use and shorten production delays. However, quoted efficiency figures often depend on test conditions. A neat spreadsheet can still mislead.
Industry standards also support a measured selection process. ISO 21360 provides methods for determining vacuum pump performance, including pumping speed and ultimate pressure. These values should be compared under similar conditions, not copied from unrelated brochures. In practical testing, engineers should record start-up time, leak-back behavior, noise, heat, and maintenance intervals. Watch the hose connections. Observe the fluid path.
This guide explains how to choose the best Vacuum Transfer Pump for real operating demands. It considers pump technology, materials, vacuum capacity, contamination risks, control systems, and lifecycle cost. Manufacturer data remains useful, but independent verification is stronger. A model may appear oversized, yet that extra capacity could protect performance when filters clog or temperatures change. Selection is rarely perfect on the first attempt. Reviewing actual operating data after installation can reveal assumptions that need correction.
Table of Contents [Hide]
What Is a Vacuum Transfer Pump and How Does It Work?
How to Choose the Best Vacuum Transfer Pump?
A vacuum transfer pump moves liquids by creating a pressure difference. The pump removes air from a sealed line or vessel. Atmospheric pressure then pushes the liquid toward the receiving side. It is not simply “sucking” liquid. That detail matters when selecting equipment.
In practical use, the pump must match the liquid, distance, temperature, and required flow rate. A thin solvent behaves differently from viscous oil or wastewater containing particles. Check the pump’s maximum vacuum, flow curve, wetted materials, and seal design. A 2024 report from Grand View Research estimated the global vacuum pump market at more than USD 5 billion, reflecting broad industrial demand. However, market size does not prove that one pump suits every process. Real operating conditions are less tidy than product tables.
Energy use also deserves attention. The U.S. Department of Energy identifies leaks, poor controls, and oversized equipment as common causes of compressed-air waste in industrial systems. Similar inefficiencies can affect vacuum transfer setups. A pump may reach deep vacuum but transfer liquid too slowly. That can increase heat, noise, and maintenance. The best choice begins with a measured test: record viscosity, suction lift, transfer volume, cycle time, and liquid temperature. Leave a safety margin. I once treated the catalog flow rate as a guaranteed result; that assumption was too optimistic. Inlet losses and hose length changed the outcome.
Which Vacuum Transfer Pump Specifications Match Your Application?
Choosing the best vacuum transfer pump starts with matching specifications to the actual application. A high vacuum rating may look impressive, but it cannot compensate for poor flow control. Define the required vacuum level, transfer speed, and operating pressure first. A pump moving thin water will behave differently with viscous oil, solvent vapors, or fine particles. Check the pump’s flow rate under working conditions, not only its maximum rating. Maximum figures can mislead.
Material compatibility is equally important. Confirm that the wetted parts resist the liquid, vapor, and cleaning agents used on site. Temperature range matters too. Hot fluids can damage seals and reduce pump life. If the process releases vapor, consider vapor tolerance and suitable filtration. I once saw a pump selected correctly on paper, yet its seal failed because the cleaning fluid was ignored. That detail was easy to miss.
Power supply, duty cycle, noise, and installation space also affect the choice. A compact pump may fit beneath a tank but struggle during continuous operation. Check whether the motor supports the available voltage and whether cooling remains adequate in a confined area. Maintenance access should be practical; awkward servicing often gets delayed. Safety features, leak control, and clear operating instructions should be verified before purchase. No specification is perfect. Leave a realistic margin for changing viscosity, temperature, and workload. Your process may be stable today, but real production rarely stays that way.
How to Choose the Best Vacuum Transfer Pump? - Which Vacuum Transfer Pump Specifications Match Your Application?
| Application | Recommended Pump Type | Typical Pumping Speed | Typical Ultimate Pressure | Gas or Material Compatibility | Recommended Inlet Protection | Temperature Considerations | Key Selection Priorities |
|---|---|---|---|---|---|---|---|
| General laboratory vacuum transfer | Oil-free diaphragm pump | 0.5–10 m³/h | Approximately 1–10 mbar absolute | Air, inert gases, and moderate chemical vapors; confirm elastomer compatibility | Vacuum filter and condensate trap | Avoid continuous condensation unless the pump is designed for it | Clean operation, low maintenance, chemical resistance, and noise level |
| Solvent evaporation and rotary evaporation | Chemical-resistant diaphragm pump | 1–8 m³/h | Approximately 1–5 mbar absolute | Organic vapors and corrosive gases, subject to wetted-material selection | Cold trap or solvent condenser upstream of the pump | Keep vapor temperature within the pump’s rated inlet range; prevent liquid slugging | Chemical resistance, vapor-handling capacity, ultimate pressure, and solvent recovery |
| High-flow air evacuation | Oil-lubricated rotary vane pump or dry scroll pump | 10–100 m³/h | Approximately 0.001–1 mbar absolute | Dry air and inert gases; oil-sealed designs require contamination control | Inlet screen, particulate filter, and suitable exhaust filtration | Use gas ballast or equivalent moisture-management features when required | Pump-down time, continuous-duty rating, ultimate pressure, and operating cost |
| Food, pharmaceutical, and hygienic transfer | Dry claw, dry screw, or oil-free diaphragm pump | 10–250 m³/h | Approximately 0.1–100 mbar absolute, depending on design | Air and process gases; select materials compatible with cleaning agents | Sanitary inlet filter, liquid separator, and cleanable piping | Consider washdown, condensate, and cleaning-cycle temperatures | Oil-free compression, cleanability, drainage, hygienic materials, and validation requirements |
| Vacuum packaging | Rotary vane, dry claw, or dry scroll pump | 20–300 m³/h | Approximately 0.5–10 mbar absolute | Air and food-related vapors; oil-free operation may be preferred | Product filter, liquid separator, and optional bacterial filter | Manage moisture and product vapor to avoid corrosion or performance loss | Cycle time, peak flow, moisture tolerance, footprint, and service intervals |
| Liquid transfer and priming | Liquid-ring pump or vacuum-assisted centrifugal system | 10–500 m³/h | Typically 30–100 mbar absolute, depending on liquid temperature | Wet gases and entrained liquids; liquid compatibility is essential | Liquid separator, non-return valve, and appropriately sized inlet piping | Water vapor pressure limits the achievable vacuum; hot liquids reduce performance | Liquid compatibility, seal design, priming time, cooling-water demand, and corrosion resistance |
| Dusty or abrasive material handling | Dry claw or rotary lobe pump with robust filtration | 20–500 m³/h | Approximately 10–200 mbar absolute | Air and dry process gases; protect the pump from abrasive solids | High-efficiency cyclone, cartridge filter, or bag filter with differential-pressure monitoring | Prevent overheating caused by blocked filters or restricted airflow | Filter area, dust-loading capacity, wear resistance, cleanout method, and shutdown protection |
| Continuous industrial vacuum service | Dry screw, dry claw, rotary vane, or liquid-ring pump | 50–2,000 m³/h | Approximately 0.1–500 mbar absolute, depending on pump technology | Select according to gas composition, moisture level, dust content, and corrosion risk | Process-specific filtration, separators, condensers, and check valves | Verify ambient, gas, cooling, and discharge temperature limits | Total cost of ownership, redundancy, energy consumption, controls, uptime, and maintenance access |
Selection note: The ranges shown are typical engineering benchmarks for vacuum transfer applications. Actual performance depends on inlet pressure, gas composition, vapor load, piping conductance, temperature, altitude, duty cycle, and system leakage. Always confirm the pump curve and material compatibility for the specific application.
How to Compare Pump Types, Materials, and Fluid Compatibility
How to Choose the Best Vacuum Transfer Pump?
Choosing a vacuum transfer pump starts with the fluid, not the catalog. Centrifugal pumps suit low-viscosity liquids and steady flow. Diaphragm pumps handle air entrainment and intermittent transfer more reliably. Rotary vane pumps can produce deeper vacuum, but their oil may contaminate sensitive fluids. Peristaltic pumps reduce contact with moving parts, although their tubing eventually fatigues. According to the U.S. Department of Energy’s Improving Pumping System Performance guide, pumping systems can represent about 25% of industrial electricity use. Efficiency matters, but compatibility matters first.
Check wetted materials against the fluid’s temperature, concentration, and cleaning chemicals. Stainless steel offers strong corrosion resistance, while polypropylene can perform well with selected aggressive chemicals. Elastomers deserve closer attention. A seal that survives water may swell in solvents. The Chemical Resistance Guide from the U.S. National Association of Corrosion Engineers emphasizes that concentration and temperature can change corrosion behavior significantly. Do not trust a general compatibility chart blindly. Real fluid samples often reveal the uncomfortable detail.
Tips: Record viscosity, vapor pressure, solids content, temperature, and required vacuum. Then request a compatibility statement from the pump manufacturer. Test the actual hose and seal materials under operating conditions. A small bench trial can expose swelling, leakage, or unexpected flow loss. I have seen specifications focus on maximum flow while ignoring suction lift. That mistake is easy to repeat. Measure the full system, including bends, filters, and hose length.
What Operating Conditions Affect Pump Performance and Service Life?
How to Choose the Best Vacuum Transfer Pump?
What Operating Conditions Affect Pump Performance and Service Life?
A vacuum transfer pump works within a narrow operating window. Inlet pressure, fluid temperature, vapor pressure, and transfer height directly affect capacity. If the vacuum level is too aggressive, the liquid may boil inside the line. This can cause unstable flow, noise, and seal damage. A field check should record pressure at the pump inlet, not only at the receiver.
Fluid properties matter just as much. High viscosity increases resistance and reduces transfer speed. Solids can scratch valves, while abrasive particles accelerate wear on diaphragms and seals. Temperature also changes viscosity and vapor pressure. The U.S. Department of Energy’s Improving Pumping System Performance reports that pumping systems may consume about 25% of industrial motor energy. Small efficiency losses deserve attention. However, that figure is a general benchmark, not a guarantee for every facility.
Service life also depends on duty cycle and maintenance quality. Frequent starts, short pauses, and dry running create thermal and mechanical stress. The European Commission’s Industrial Vacuum Pumps preparatory studies identify energy use, leakage, and operating conditions as important performance factors. Operators should inspect filters, hoses, check valves, and seal condition at defined intervals. One common mistake is selecting capacity from a catalog alone. Real fluid temperature, vapor load, contamination, and line length can change the result. Even experienced teams sometimes overlook the effect of a partially blocked filter. Records should compare expected flow with measured flow under actual working conditions.
How to Select, Install, and Maintain the Right Vacuum Transfer Pump
Choosing a vacuum transfer pump starts with the material, not the motor size. Record viscosity, temperature, vapor pressure, solids content, required flow, and lifting height. A pump that handles water may struggle with foamy chemicals or thick oils. The U.S. Department of Energy’s Improving Pumping System Performance report states that pumping systems can consume nearly 20% of industrial electricity. Correct sizing matters.
During installation, keep suction lines short, rigid, and free from sharp bends. Place a receiver near the source to reduce liquid carryover. Install a suitable filter, check valve, drain, and pressure gauge. Confirm every seal and hose matches the fluid and temperature. Poor layout causes air leaks, unstable transfer, and unnecessary cycling. In practice, installers sometimes focus on rated flow and overlook vapor behavior. That mistake can be expensive.
Tips: Select capacity from real operating data, including peak demand. Leave reasonable margin, but avoid major oversizing. Before commissioning, test the vacuum level, transfer time, noise, and motor temperature. Maintain filters and seals on a schedule based on hours and contamination. The ISO 21360 series provides standardized methods for measuring vacuum-pump performance, helping users compare test results more reliably. Keep a simple log. Record leaks, oil condition, vibration, and unusual odors. Small changes often appear before failure.
How to Choose the Best Vacuum Transfer Pump?
Select a pump by comparing the required ultimate pressure with the process conditions, gas compatibility, flow demand, installation environment, and maintenance requirements. The chart below shows representative typical ultimate pressures for common vacuum pump technologies.
How to use this chart: Lower absolute pressure indicates a deeper vacuum. Liquid-ring and diaphragm pumps are commonly selected for moderate vacuum duties and contaminated gases, while dry-scroll and rotary-vane pumps are suitable when a deeper vacuum is required. Confirm the actual operating point, vapor load, temperature, filtration, and manufacturer specifications before installation.
| Pump technology | Typical ultimate pressure | Typical selection consideration |
|---|---|---|
| Liquid-ring | 30 mbar absolute | Handles wet or condensable gases; requires liquid management. |
| Diaphragm | 1 mbar absolute | Oil-free operation and good chemical resistance; moderate vacuum depth. |
| Dry scroll | 0.01 mbar absolute | Clean, oil-free vacuum; protect the inlet from liquid and particles. |
| Rotary-vane | 0.001 mbar absolute | Deep vacuum capability; oil condition and exhaust filtration require regular attention. |
Article Source:
What Can We Help You With?
CALL NOW TO ORDER
NH: 603-434-6911MA: 508-754-3030ME: Regular weekly deliveries from NH
CALL NOW TO ORDER
NH: 603-434-6911MA: 508-754-3030ME: Regular weekly deliveries from NH


Featured Product
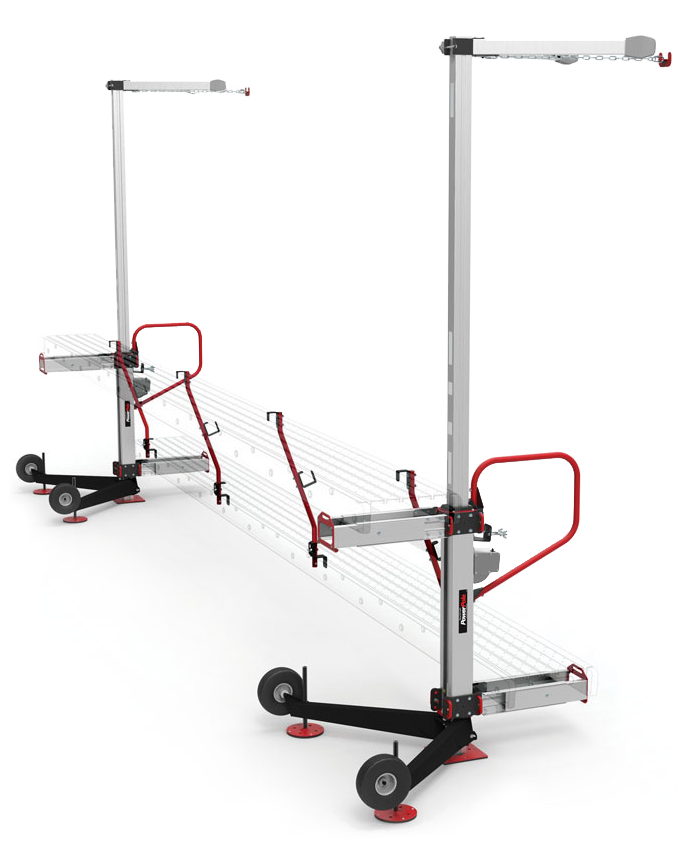
Streamlined. Safe. Flexible.
With the ReechCraft PowerPole, traditional scaffolding and pump jack systems are a thing of the past. Our streamlined design gains you access between buildings, on rooftops, around landscaping, and more. The PowerPole is perfect for contract work on residential areas.
See Products & Accessories
- ReechCraft Power Pole
- ReechCraft 4022465 – 10 in. x 10 in. Base Foot
- ReechCraft Platform Support
- ReechCraft 4022179 – Platform Support with PowerLatch Connector
- ReechCraft PowerLatch Assembly
- ReechCraft 4022084 – PowerPole 12 ft Pole Section
- ReechCraft 4022435 – PowerPole 6 ft Pole Section
- ReechCraft 4028334 – PowerPole Climbing Unit
- ReechCraft 4022096 – PowerPole Coupler
- ReechCraft 4022629 – PowerPole Extendable V-Brace
- ReechCraft 4022791 – PowerPole Outrigger
- ReechCraft 4022432 – PowerPole Standoff Tie
- ReechCraft 4022178 – PowerPole Super Standoff Tie
- ReechCraft 4022629 – PowerPole V-Brace
- ReechCraft 4022756 – Single Man Basket
- ReechCraft 4022071 – SpeedRail Endrail (Two-Pack)
- ReechCraft 4022765 – SpeedRail Midrail Post (Two-Pack)

Headache Racks That Turn Heads


See Products & Accessories
June 2022 - Month Long Promotion
Buy any of the listed Werner ladders and get
$1 Off Per Foot
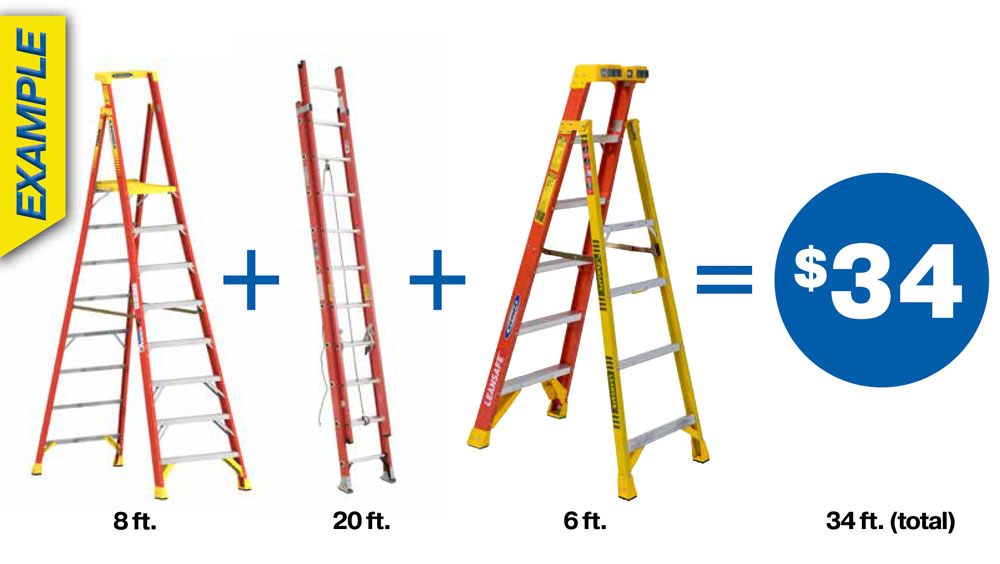
Demo and Safety Day
Don't miss our WernerCo Sfety and Demo Day BBQ
June 23rd, 2022 from 10am - 2pm
Chance to win giveaways
Cookout from 10am - 2pm
Werner fall protection and Weatherguard Specialists on site to answer any questions and perform safety and product demonstrations.
System One Modular Truck Equipment for New Hampshire, Massachusetts, Connecticut, Rhode Island, Vermont, and Maine Contractors
- Lewiston, ME
- Bar Harbor, ME
- Lexington, MA
- North Andover, MA
- East Hampton, CT
- Meredith, NH
- Concord, NH
- Bennington, VT
- Biddeford, ME
- West Fairlee, VT
- Hopkinton, RI
- Freeport, ME
- Danbury, CT
- Waterboro, ME
- Winslow, ME
- Buxton, ME
- Southington, CT
- Milford, NH
- Pownal, VT
- South Berwick, ME
- North Haven, CT
- Atkinson, NH
- Farmington, NH
- Whitingham, VT
- Pelham, NH
- Essex, VT
- Wallingford, VT
- Laconia, NH
- Narragansett, RI
- Fair Haven, VT
- Sandown, NH
- New London, NH
- Portsmouth, RI
- Haverhill, NH
- Needham, MA
- Bridgewater, MA
- Middletown, RI
- Montpelier, VT
- Barre, VT
- St. Johnsbury, VT
- Livermore Falls, ME
- Sandwich, MA
- Newport, RI
- Raymond, NH
- Tunbridge, VT
- Barnet, VT
- Brooksville, ME
- Gorham, ME
- Litchfield, ME
- Bristol, CT
- Rumford, ME
- Thompson, CT
- Dover, VT
- Westminster, VT
- Waitsfield, VT
- Torrington, CT
- Scituate, RI
- Barnstead, NH
- Lovell, ME
- Barton, VT
- Unity, ME
- Skowhegan, ME
- Groton, CT
- Northfield, VT
- Hopkinton, NH
- Limerick, ME
- Candia, NH
- Berwick, ME
- Killington, VT
- Peacham, VT
- North Hampton, NH
- Randolph, MA
- Bloomfield, CT
- Watertown, MA
- Wilmington, MA
- Methuen, MA
- Nashua, NH
- Plymouth, NH
- Newmarket, NH
- Alfred, ME
- Caribou, ME
- Weymouth, MA
- North Yarmouth, ME
- Bethel, CT
- Rocky Hill, CT
- Bristol, RI
- Sabattus, ME
- Salem, MA
- Londonderry, NH
- Chester, NH
- Westford, VT
- Stamford, CT
- Vershire, VT
- East Hartford, CT
- Norwich, CT
- Stratham, NH
- Windham, NH
- Vernon, CT
Knaack Jobsite Boxes, Chests, Cabinets, Workbenches, Field Offices, and Accessories
- Raymond, ME
- Fairfax, VT
- Presque Isle, ME
- Highgate, VT
- Norridgewock, ME
- Old Saybrook, CT
- Marblehead, MA
- Nashua, NH
- Mashpee, MA
- Auburn, NH
- Bowdoin, ME
- Milford, CT
- Bolton, CT
- Mendon, VT
- Dartmouth, MA
- Portland, CT
- North Haven, CT
- New Gloucester, ME
- Bourne, MA
- New Canaan, CT
- Belmont, NH
- Rutland, VT
- Fitchburg, MA
- Waterbury, CT
- Burlington, VT
- Fair Haven, VT
- Bethel, VT
- Greene, ME
- Chicopee, MA
- New London, CT
- Gloucester, MA
- Mechanic Falls, ME
- Wilmington, MA
- Fairfield, CT
- Methuen, MA
- Newport, ME
- Bakersfield, VT
- Monroe, CT
- Meriden, CT
- Prospect, CT
- Thomaston, ME
- Watertown, MA
- Winchester, ME
- Hampstead, NH
- Gilford, NH
- Pownal, VT
- Essex Junction, VT
- Lincoln, ME
- East Lyme, CT
- Tolland, CT
- Naugatuck, CT
- Dennis, MA
- Waldoboro, ME
- Derry, NH
- Bridgewater, MA
- Windham, NH
- Longmeadow, MA
- West Rutland, VT
- Warren, ME
- Coventry, RI
- Whitingham, VT
- Bow, NH
- Norway, ME
- Smithfield, RI
- Sharon, VT
- Amherst, MA
- Wells, ME
- Sabattus, ME
- Stoughton, MA
- Thetford, VT
- Tewksbury, MA
- Norwich, CT
- Rochester, VT
- Gray, ME
- Madison, ME
- Leominster, MA
- Newington, CT
- Sutton, VT
- Shelton, CT
- East Hampton, CT
- Darien, CT
- Haverhill, NH
- Houlton, ME
- Foster, RI
- Medford, MA
- Littleton, NH
- Seymour, CT
- Harrisville, RI
- Killingworth, CT
- Bellows Falls, VT
- Lunenburg, VT
- Saco, ME
- Peterborough, NH
- Frankfort, ME
- Albany, VT
- Plainville, CT
- North Kingstown, RI
Thule TracRac from the Thule TracRac Resellers New England Trusts
- South Windsor, CT
- Melrose, MA
- Manchester, CT
- Limerick, ME
- Glocester, RI
- South Portland, ME
- Brookline, NH
- Killingworth, CT
- Thompson, CT
- Groton, CT
- Montgomery, VT
- Mendon, VT
- Derby, VT
- Newington, CT
- Somersworth, NH
- West Haven, CT
- Merrimack, NH
- Bellows Falls, VT
- South Berwick, ME
- Gorham, ME
- Marblehead, MA
- Hudson, MA
- Alton, NH
- Jericho, VT
- Simsbury, CT
- Skowhegan, ME
- Plaistow, NH
- North Andover, MA
- Camden, ME
- Brookfield, CT
- Vergennes, VT
- Pittsfield, ME
- Hartford, VT
- Sanford, ME
- Swanzey, NH
- Kingston, NH
- Alfred, ME
- Needham, MA
- West Springfield, MA
- Underhill, VT
- Middletown, CT
- Amherst, NH
- Sidney, ME
- Natick, MA
- South Kingstown, RI
- Vershire, VT
- Richmond, ME
- Quincy, MA
- Bolton, CT
- Hallowell, ME
- West Hartford, CT
- Wardsboro, VT
- Avon, CT
- Bridgeport, CT
- Sudbury, MA
- Waltham, MA
- Marion, MA
- Waterbury, CT
- Southbury, CT
- Vernon, CT
- Warwick, RI
- Pembroke, NH
- Leominster, MA
- Torrington, CT
- Weare, NH
- Barrington, NH
- New Bedford, MA
- Charlestown, RI
- Jefferson, ME
- Pittsfield, MA
- Newport, NH
- Madison, ME
- Providence, RI
- Brookline, MA
- South Hadley, MA
- Barnstead, NH
- Peabody, MA
- Madison, CT
- Raymond, ME
- Barre, VT
- Augusta, ME
- Belmont, MA
- Ellington, CT
- Cambridge, MA
- Claremont, NH
- Falmouth, MA
- North Yarmouth, ME
- Norridgewock, ME
- Ipswich, MA
- East Providence, RI
- Johnston, RI
- Bedford, NH
- Scituate, RI
- Huntington, VT
- Seabrook, NH
- Danville, VT
- Clinton, CT
- Eliot, ME
Purchase Alum-A-Pole Products from Nation Wide Ladder – Ladder Distributors in MA, NH, CT, ME, VT, and RI
- Providence
- Cranston
- Warwick
- Pawtucket
- East Providence
- Woonsocket
- Newport
- Central Falls
- Manville
- Harrisville
- Burlington
- Barre
- South Burlington
- Rutland
- Essex Junction
- St Albans
- Montpelier
- Winooski
- Bellows Falls
- Newport
Purchase 28 Ft Extension Ladders from Nation Wide Ladder – Ladder Distributors in MA, NH, CT, ME, VT, and RI
- Providence
- Cranston
- Warwick
- Pawtucket
- East Providence
- Woonsocket
- Newport
- Central Falls
- Manville
- Harrisville
- Burlington
- Barre
- South Burlington
- Rutland
- Essex Junction
- St Albans
- Montpelier
- Winooski
- Bellows Falls
- Newport
Purchase 40 Ft Extension Ladders from Nation Wide Ladder – Ladder Distributors in MA, NH, CT, ME, VT, and RI
- Providence
- Cranston
- Warwick
- Pawtucket
- East Providence
- Woonsocket
- Newport
- Central Falls
- Manville
- Harrisville
- Burlington
- Barre
- South Burlington
- Rutland
- Essex Junction
- St Albans
- Montpelier
- Winooski
- Bellows Falls
- Newport
Purchase 28 Ft Fiberglass Extension Ladders from Nation Wide Ladder – Ladder Distributors in MA, NH, CT, ME, VT, and RI
- Providence
- Cranston
- Warwick
- Pawtucket
- East Providence
- Woonsocket
- Newport
- Central Falls
- Manville
- Harrisville
- Burlington
- Barre
- South Burlington
- Rutland
- Essex Junction
- St Albans
- Montpelier
- Winooski
- Bellows Falls
- Newport